An acid shortage, and no room to stop
A countrywide shortage of sulfuric acid was taking place during a higher oil refinery production period. This meant a large oil refinery in Germany could not regenerate its own ion-exchange (IX) resin as normal. A continuous delivery of high-purity water is critical for steam generation, cooling, and process applications at the refinery. Any disruption could force reductions in throughput or unplanned refinery shutdowns.
The refinery urgently sought to integrate temporary brackish water reverse osmosis (RO) systems into its existing water treatment process. With production at full capacity the installation had to be completed without any disruption to the refinery operations.
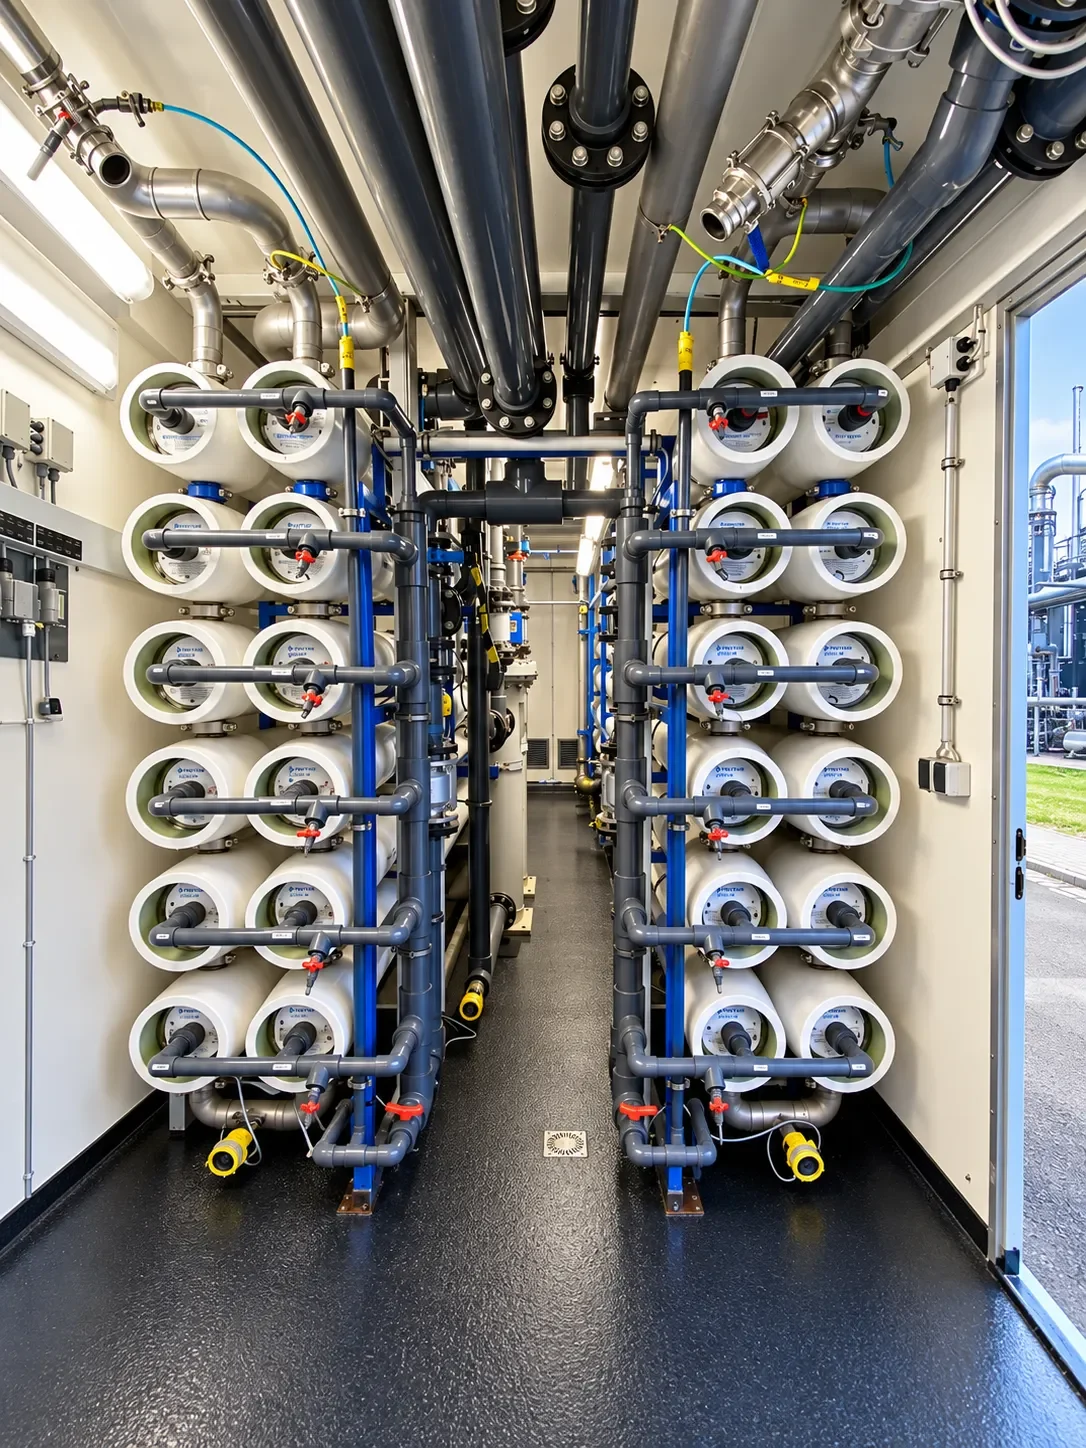
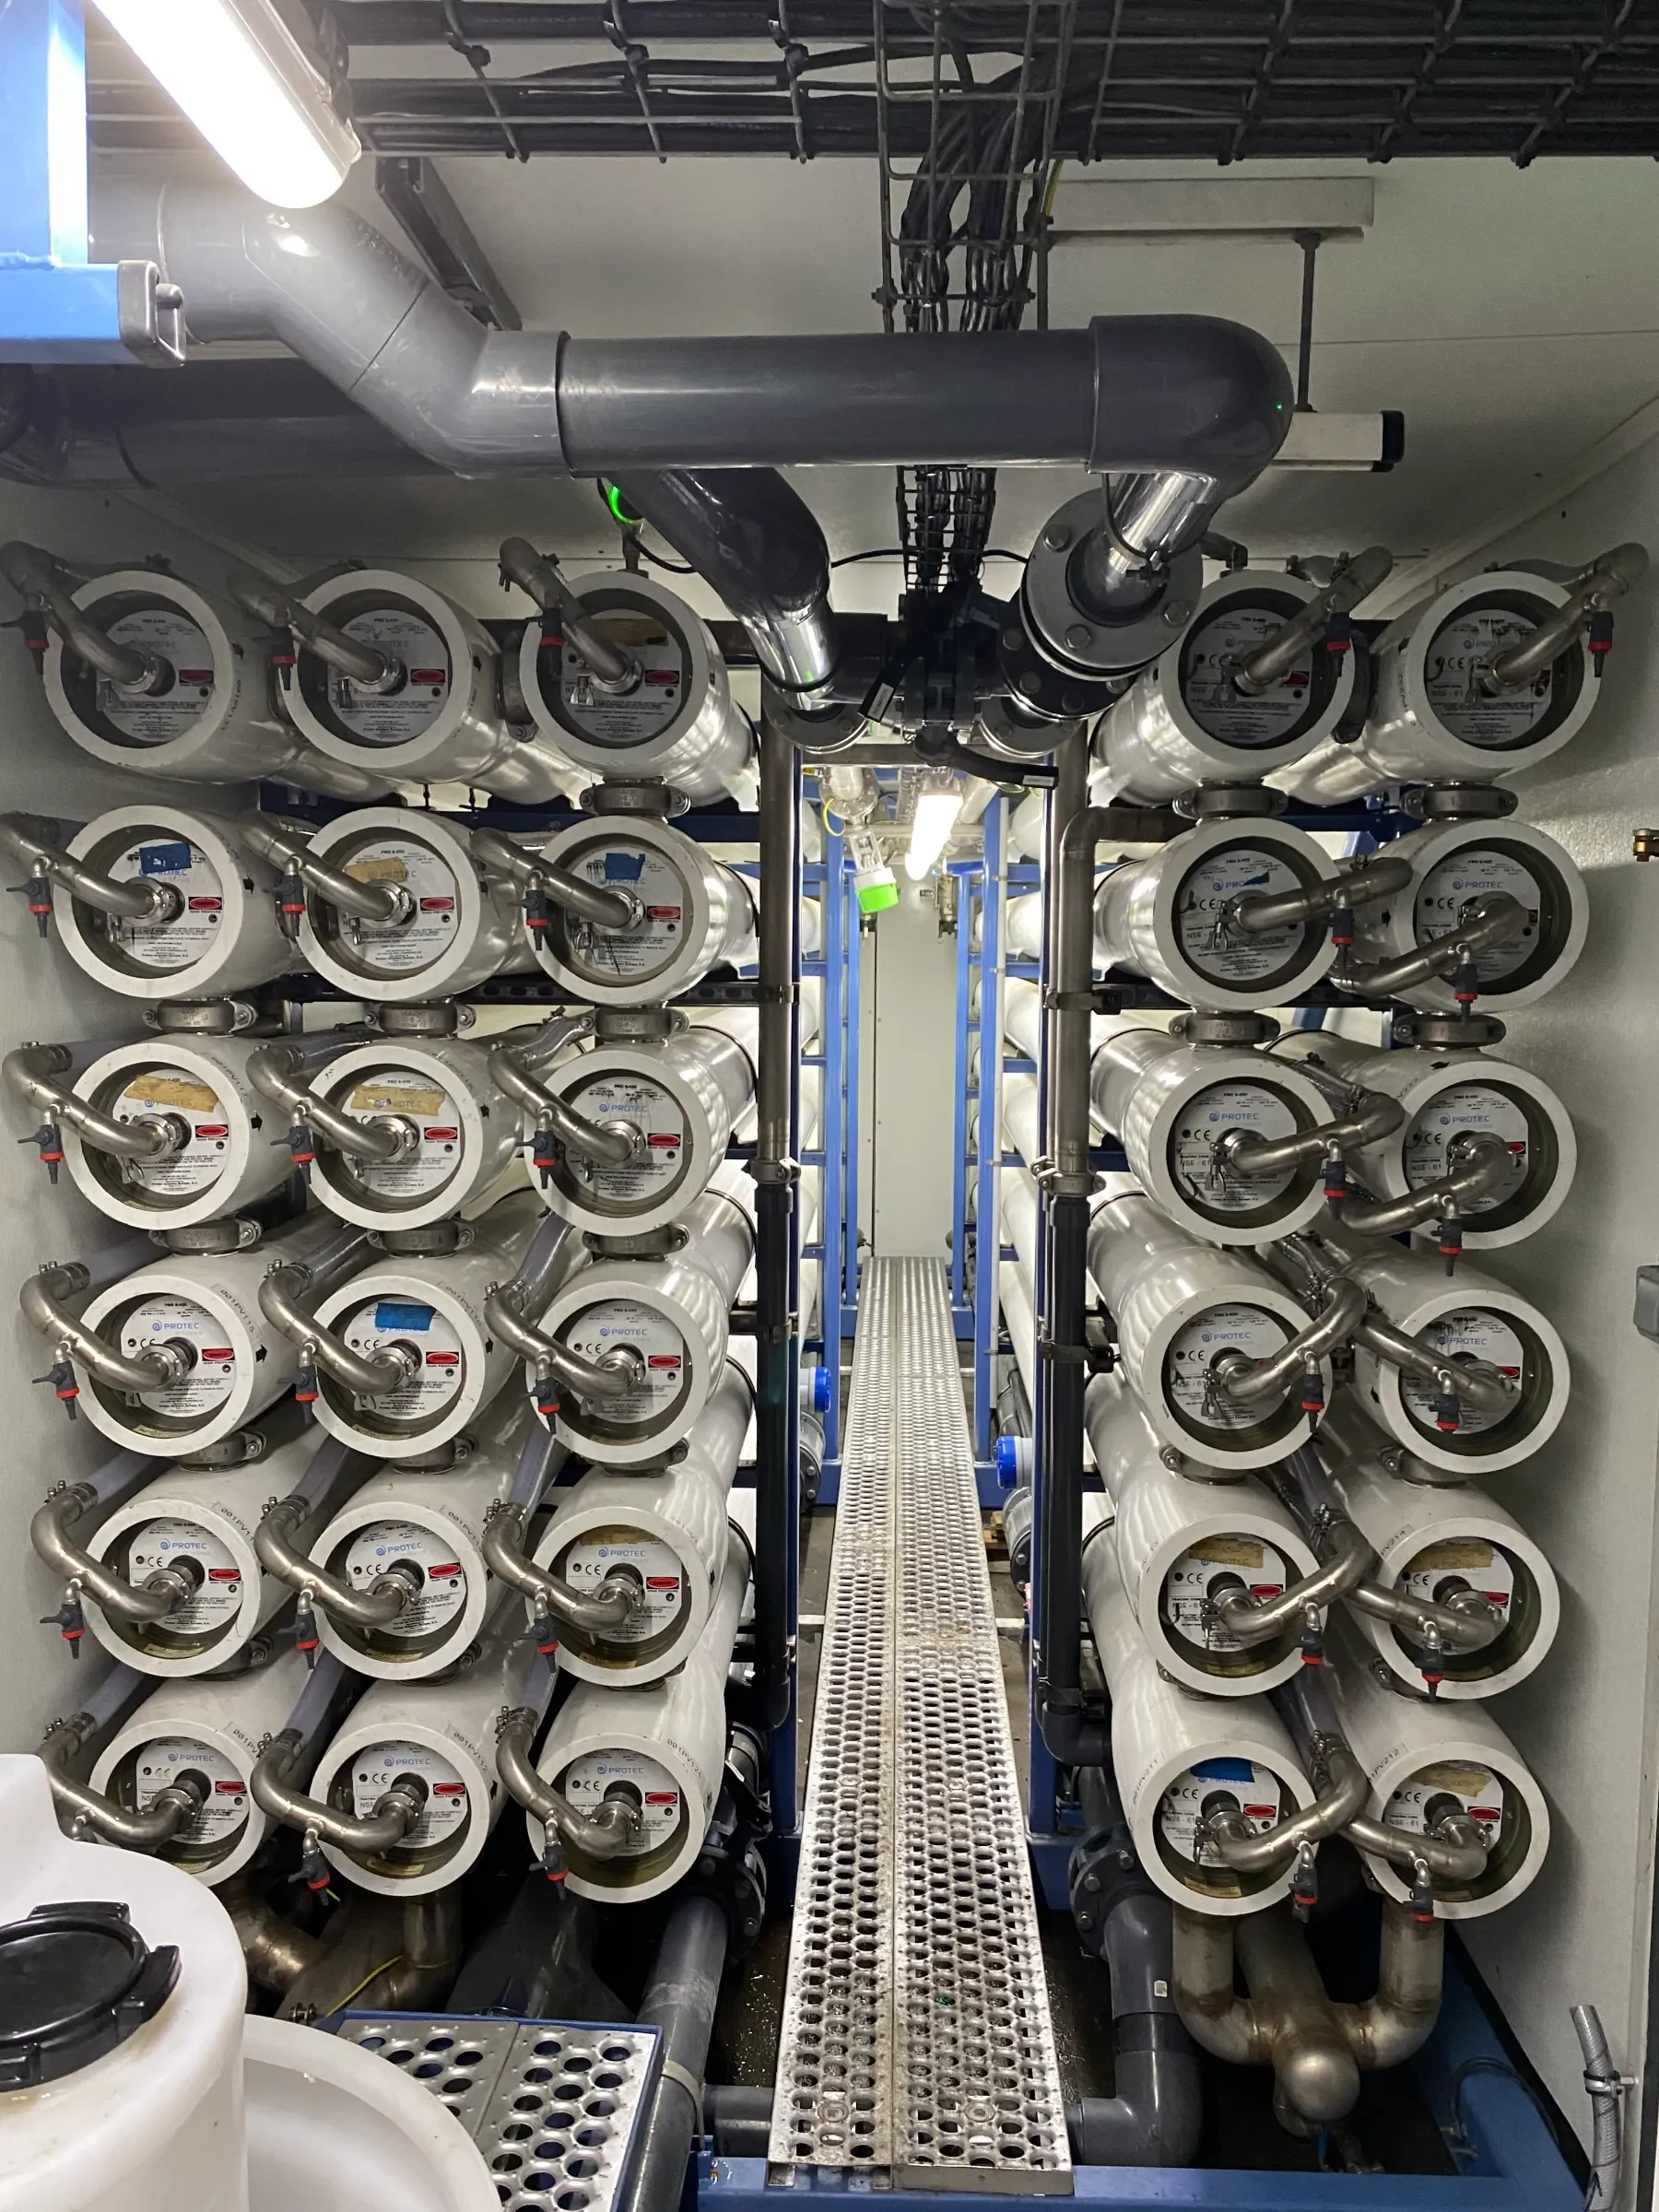
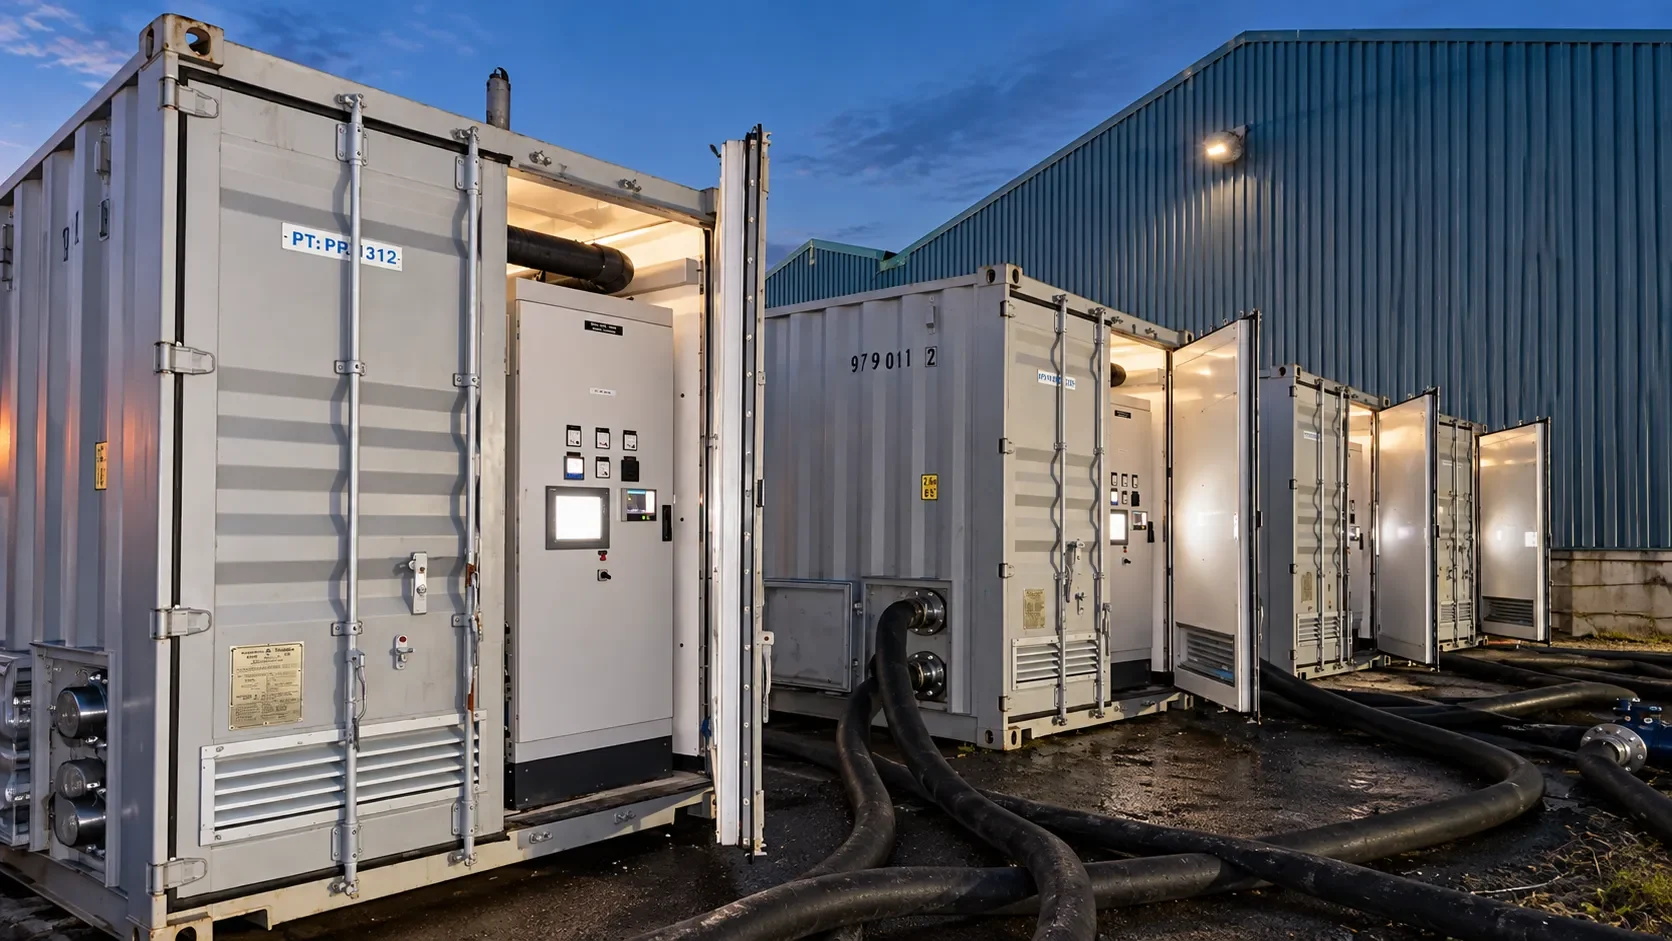
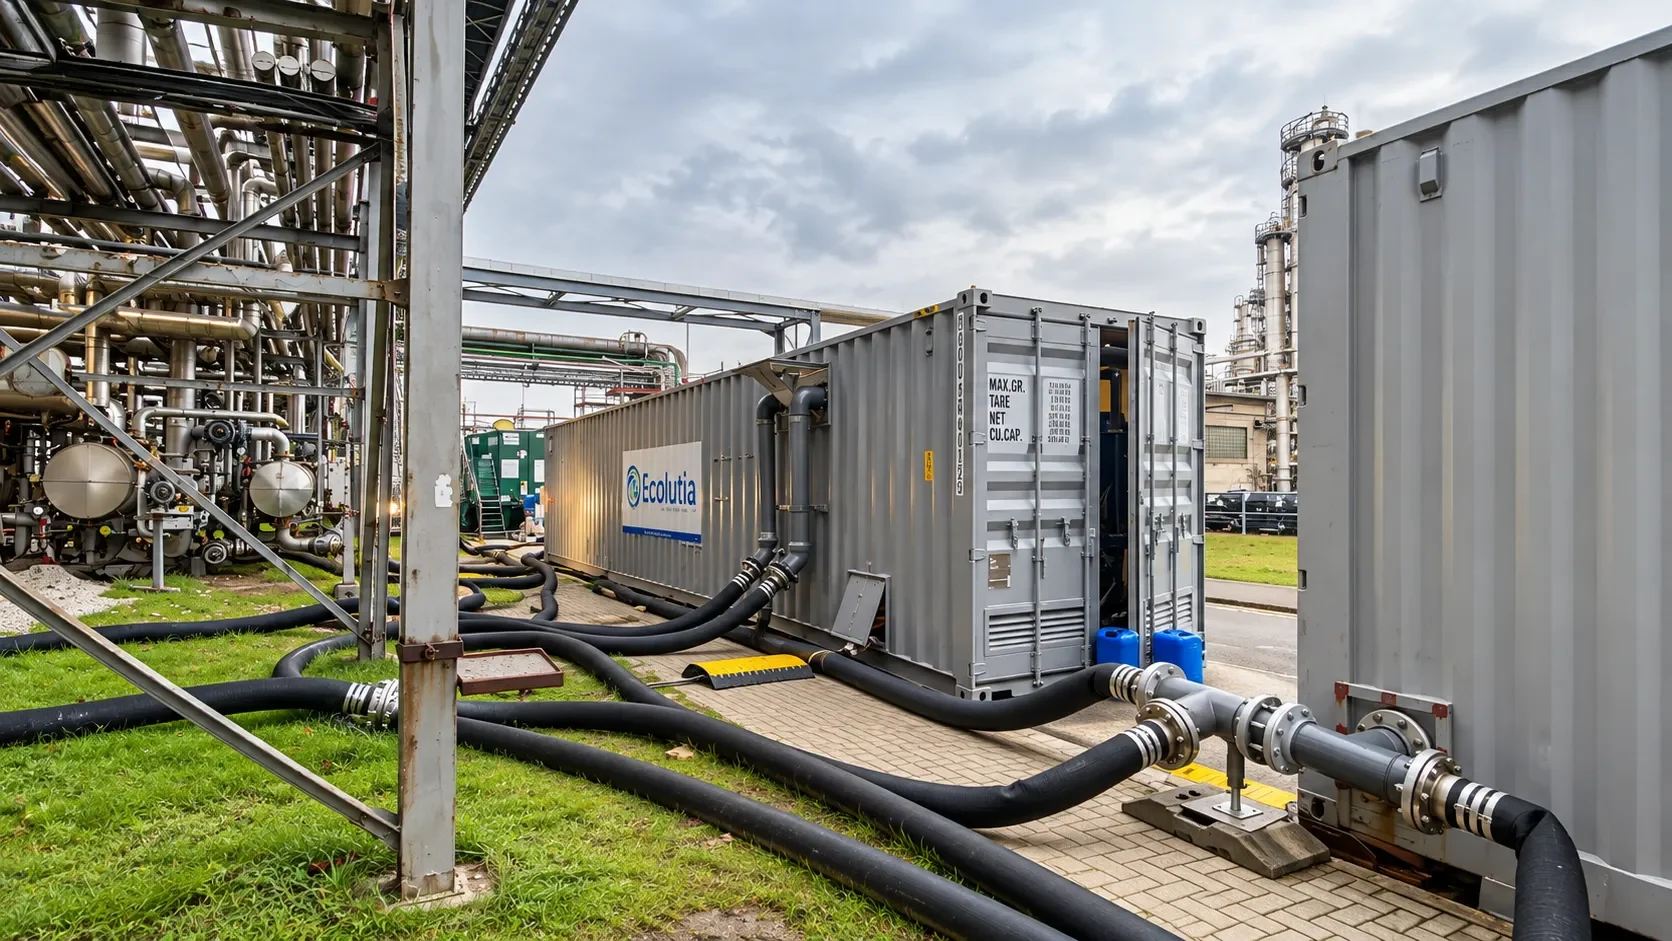
Three mobile RO units integrated within a live operational refinery
Ecolutia smoothly integrated three Triton BWRO96 reverse osmosis systems into the onsite water treatment process. Operational within a few days in a parallel configuration, the high-quality RO permeate, at a flowrate of 800 GPM, ensures refinery operations are not disrupted.
Integrating between the onsite filtration and ion-exchange systems allows the ROs to receive a filtered municipal feedwater with lower NTU and SDI levels. This supports high-quality RO permeate production, so the downstream ion-exchange system can run at full capacity with the advantage of regenerating the resin less frequently, thereby significantly reducing chemical and manpower needs.
Precise timings and communication between Ecolutia and refinery engineers were the key to avoid disruption to the water treatment process and other onsite operations. Scheduling backwashes of the upstream filtration feeding the Ecolutia ROs was essential to maintain sufficient pressure and flow within the units so downstream water production could continue.
Six months planned, twelve months delivered
The initial planned 6-month project was a success and helped improve demineralized water production, such that the customer signed a 6-month extension.
The RO permeate consistently produced water with >95% contaminant rejection at flows of 800 GPM, 24 hours a day, 7 days a week. This ensured minimal disruption and downtime to the customer’s process, allowing them to focus on other on-site activities.
The remote monitoring system Ecolutia employs has enabled rapid response times when the customer has requested a change in flow conditions, as well as the ability to monitor the process while off-site to ensure a smooth operation.