The role of water in textile manufacturing
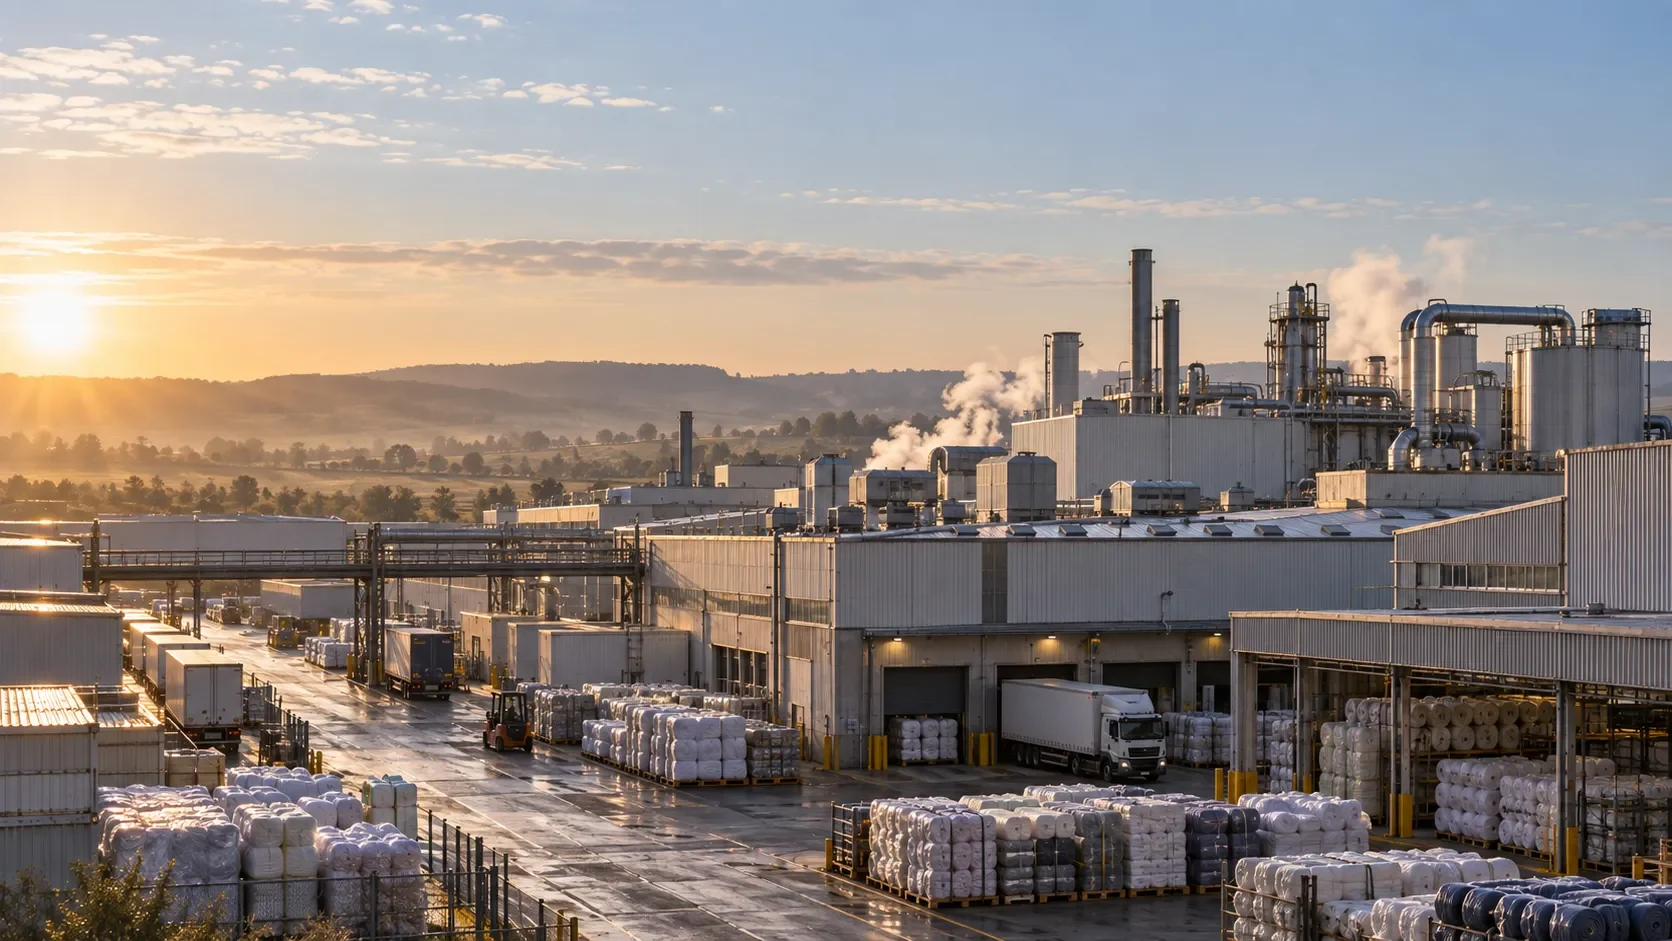
Water is fundamental to textile production — from fibre preparation and dyeing to washing, finishing and steam generation. In high-throughput plants, water quality directly affects colour consistency, fabric quality, chemical performance, energy efficiency and environmental compliance.
Facilities rely on treated water across many process and utility applications, where consistent quality and access is essential for large-scale garment production.
Technology solutions we deploy
Mobile systems configured around your plant's feedwater profile, dye chemistry, flow requirements, steam demand and discharge limits.
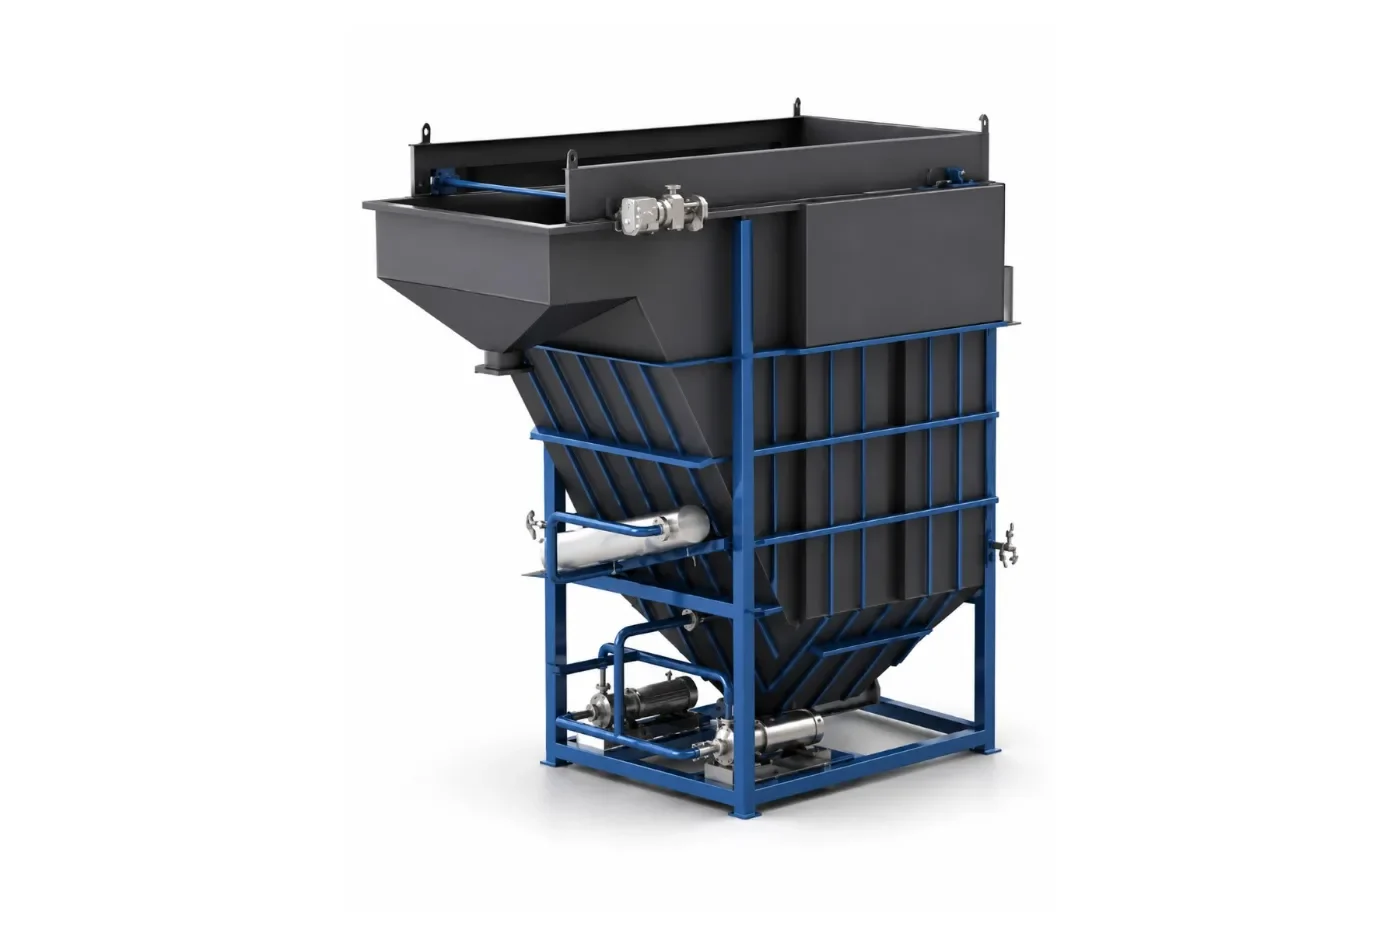
Enhanced treatment for solids and colour removal.
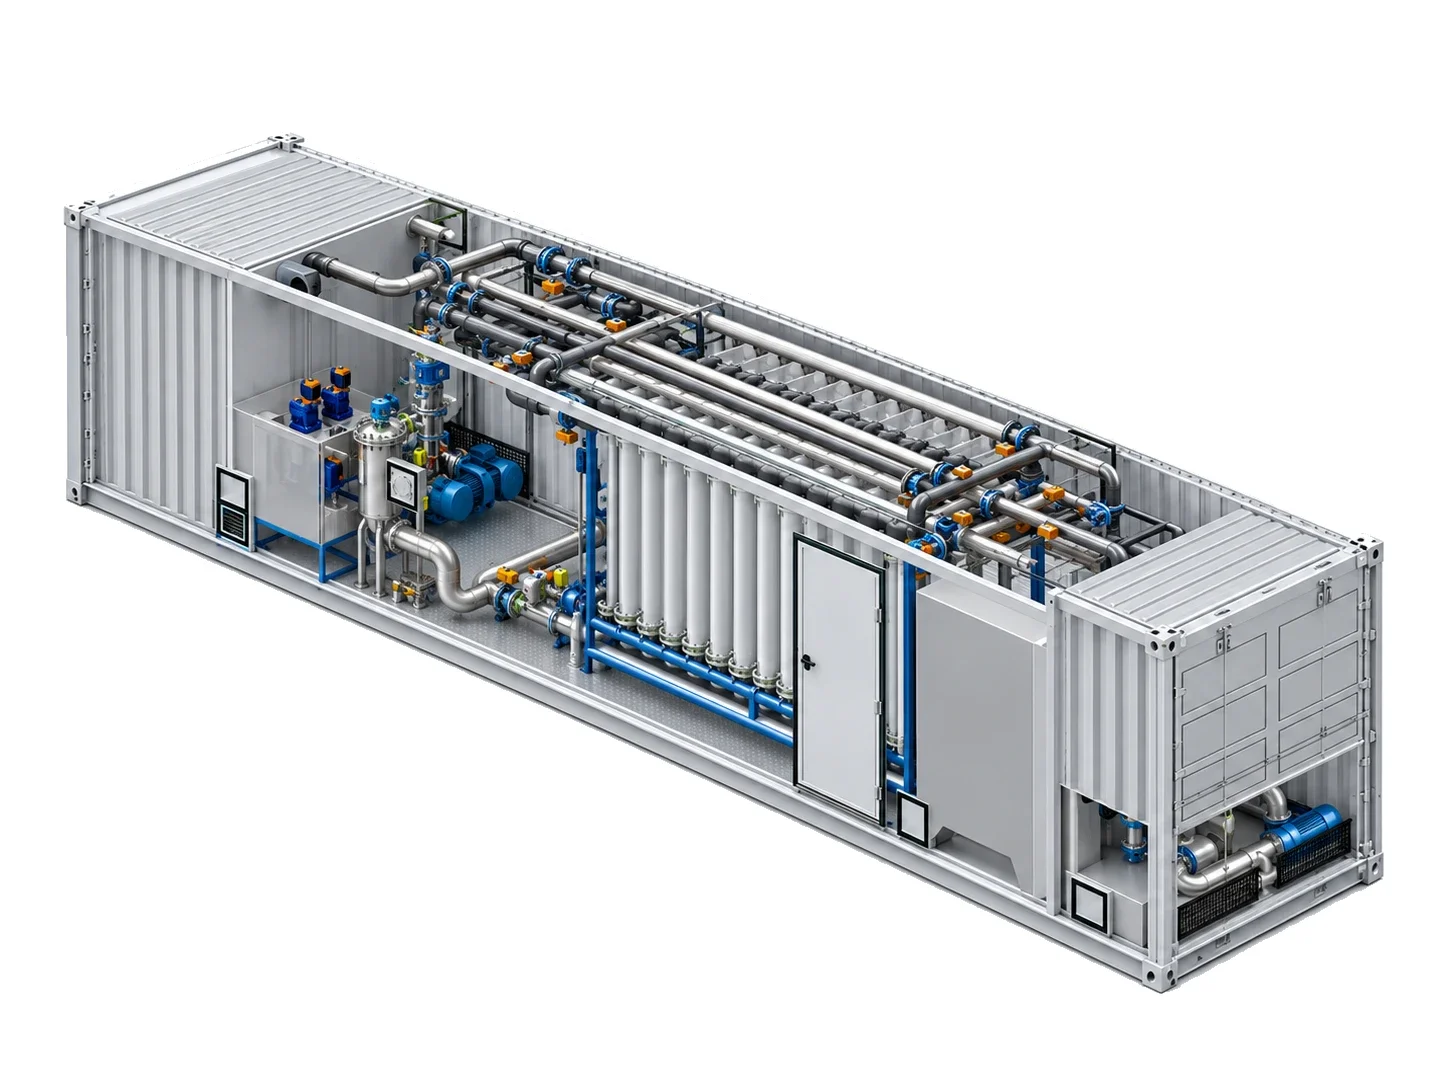
Membrane pre-treatment for suspended solids and organics.
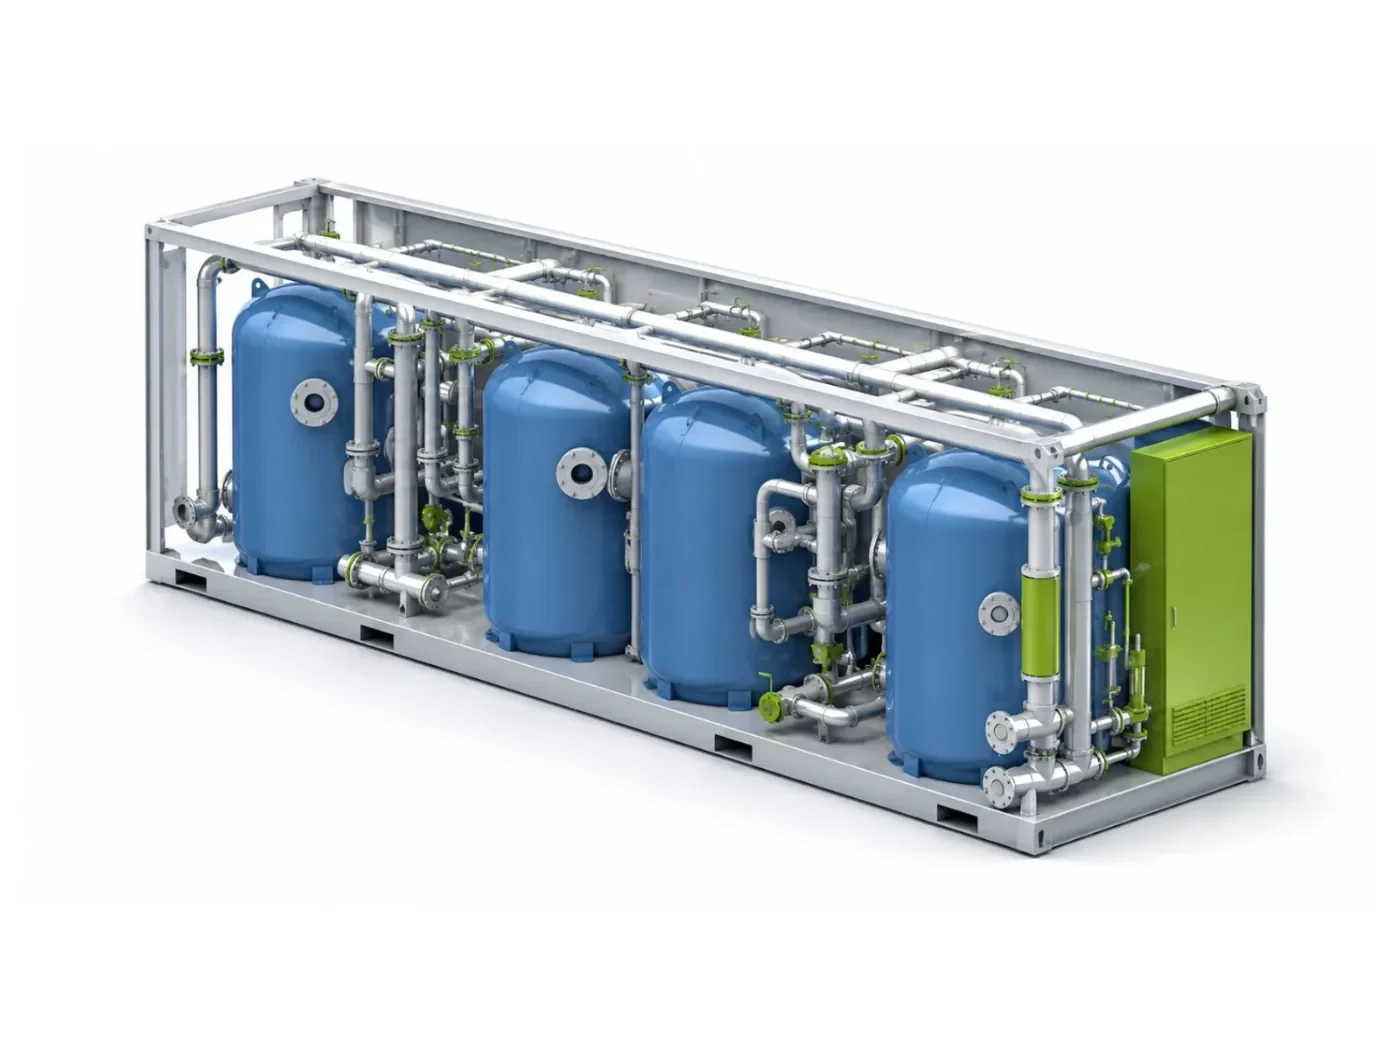
Protection of steam cycle chemistry using multi-media filtration.
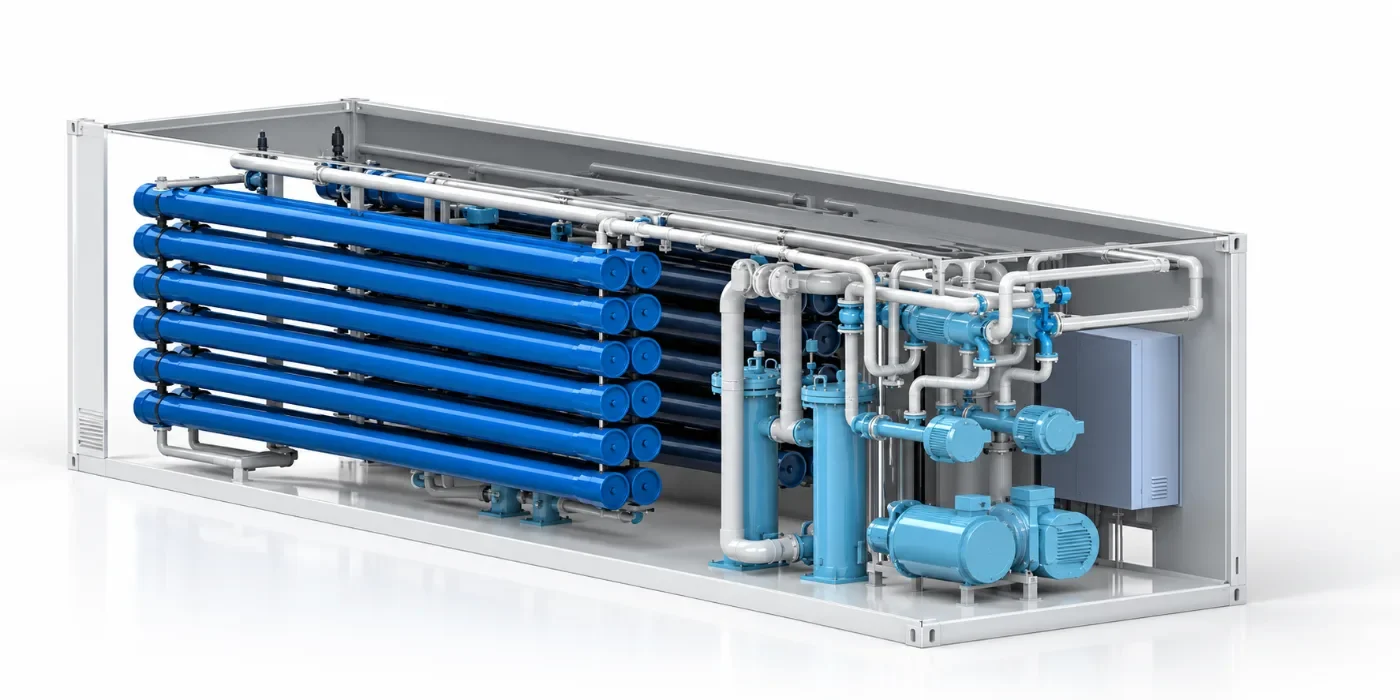
High-purity water production from seawater.
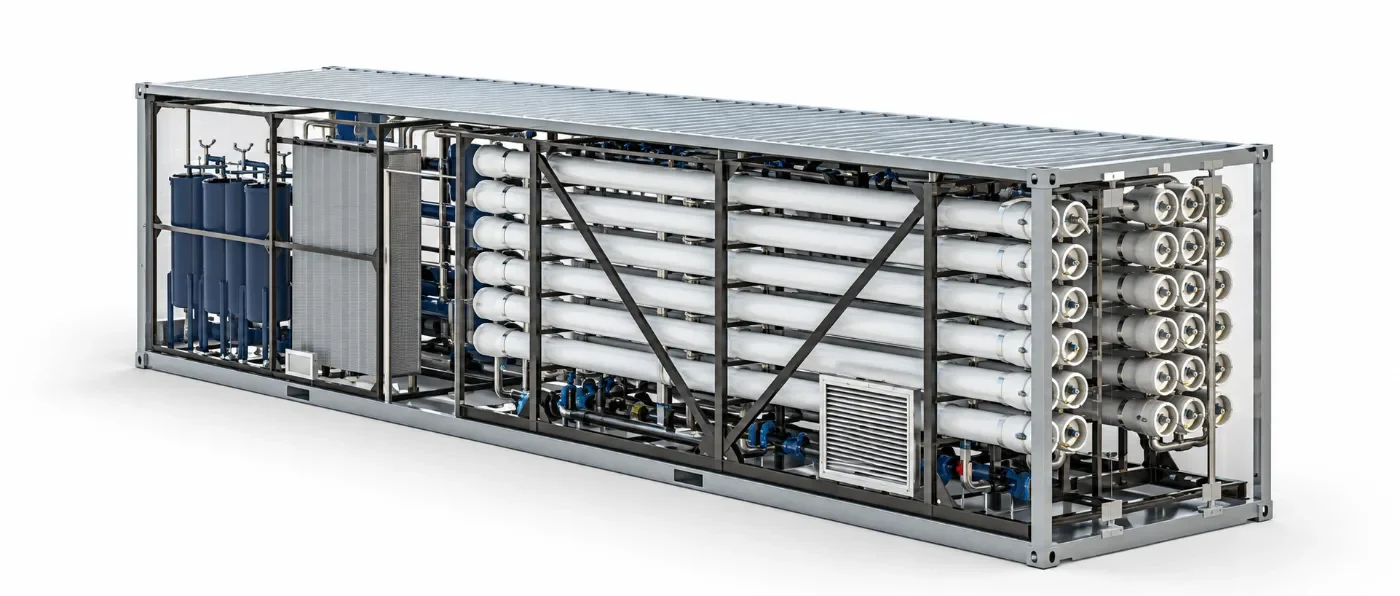
High-purity water with dissolved salts and hardness removed.
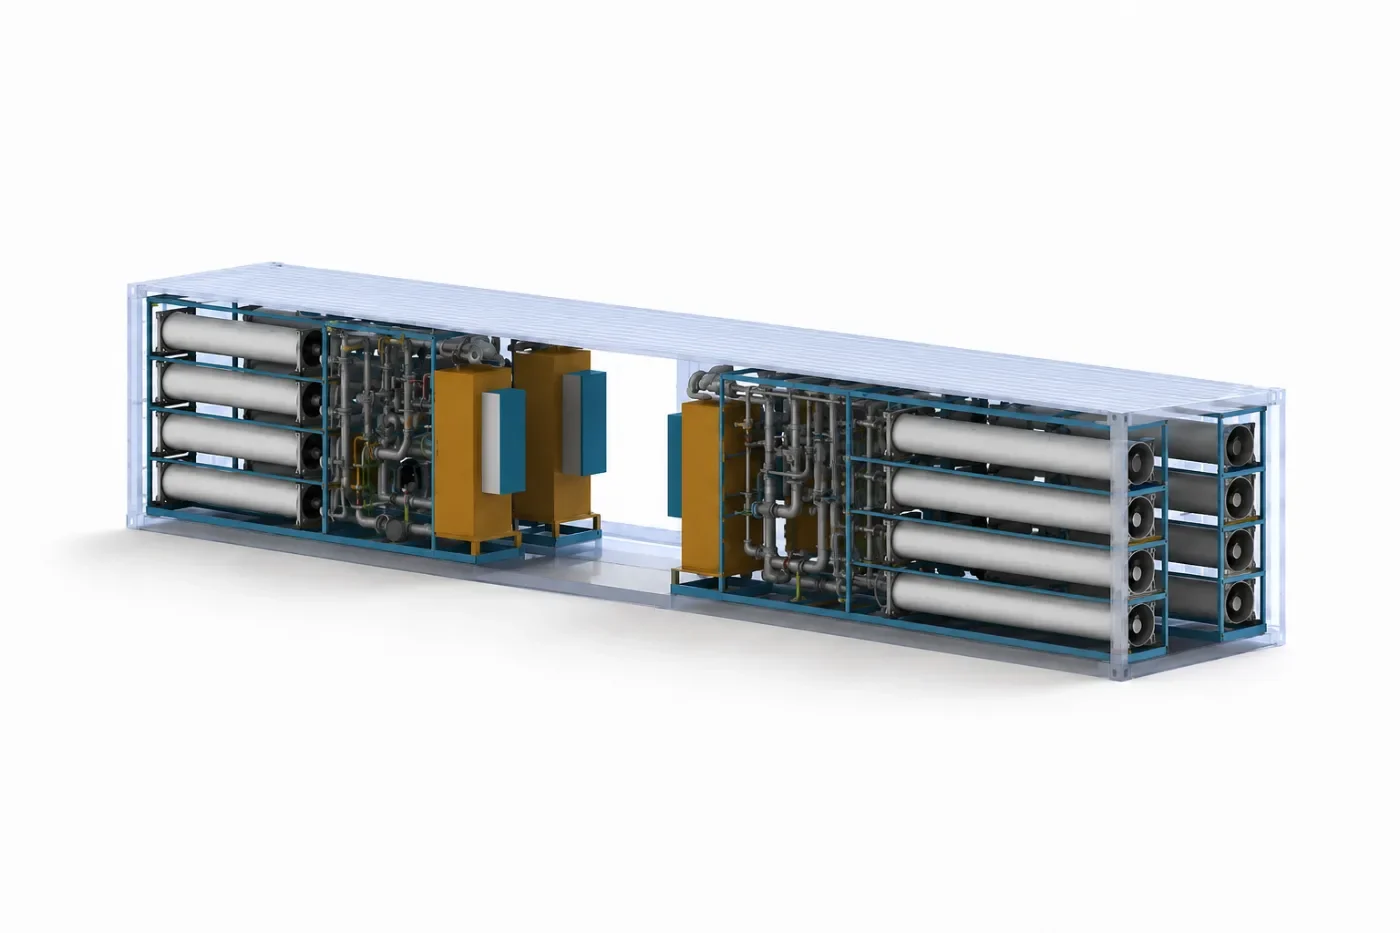
Continuous high-purity demineralised water without regenerants.
Benefits for textile manufacturers
During quality or system failures.
Improved product uniformity.
Boilers, exchangers and vessels.
Reduced environmental risk.
Aligned to seasonal cycles.
Service-based solutions.
Frequently asked questions
From emergency response and seasonal capacity to long-term water management — these are the questions textile manufacturers ask us most.