The whole refinery’s oily water, with the DAF out of service
One of the largest refineries in Spain faced a critical operational challenge: it needed a reliable temporary bypass to provide pretreatment whilst planned maintenance of its own DAF was carried out. This pretreatment stage plays a vital role in the plant’s operations, treating oily and greasy wastewater generated across the entire refinery.
The maintenance work required careful coordination among numerous operators and contracting companies, all working together to complete the intervention as efficiently and quickly as possible — without compromising environmental compliance or process continuity.
The challenge was further heightened by the demanding and variable characteristics of the feed water, which required a solution capable of handling:
These conditions demanded a robust, high-capacity solution capable of stepping in seamlessly, ensuring the refinery could maintain full operational continuity throughout the maintenance period.
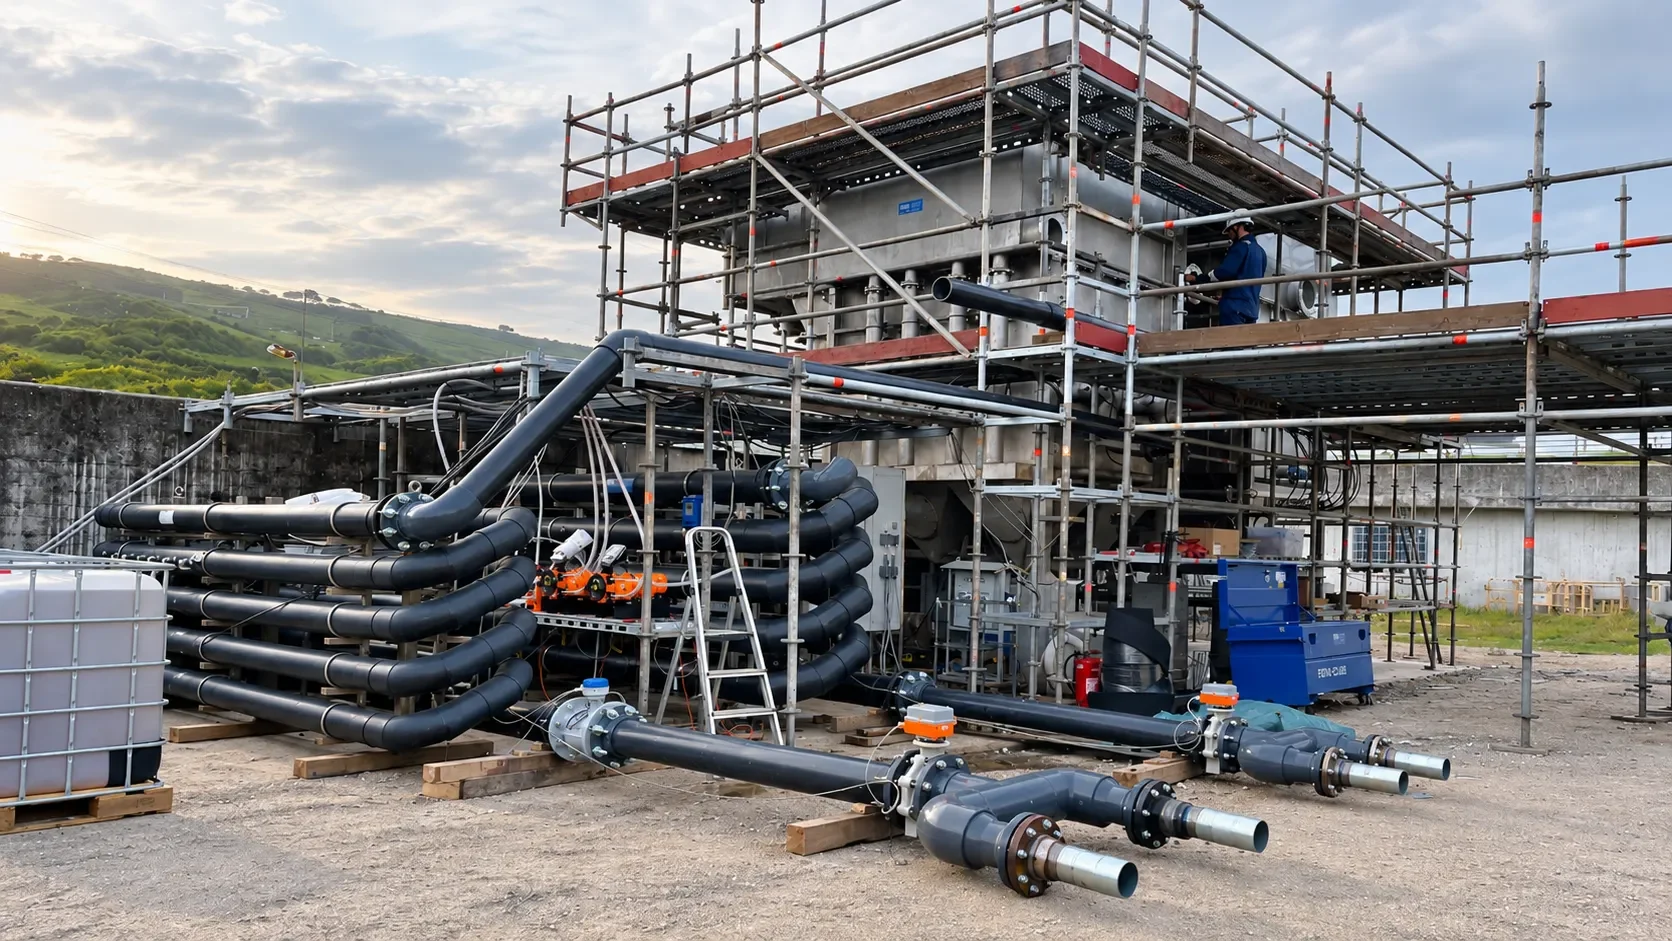
Two DAF trains, routed to run on gravity
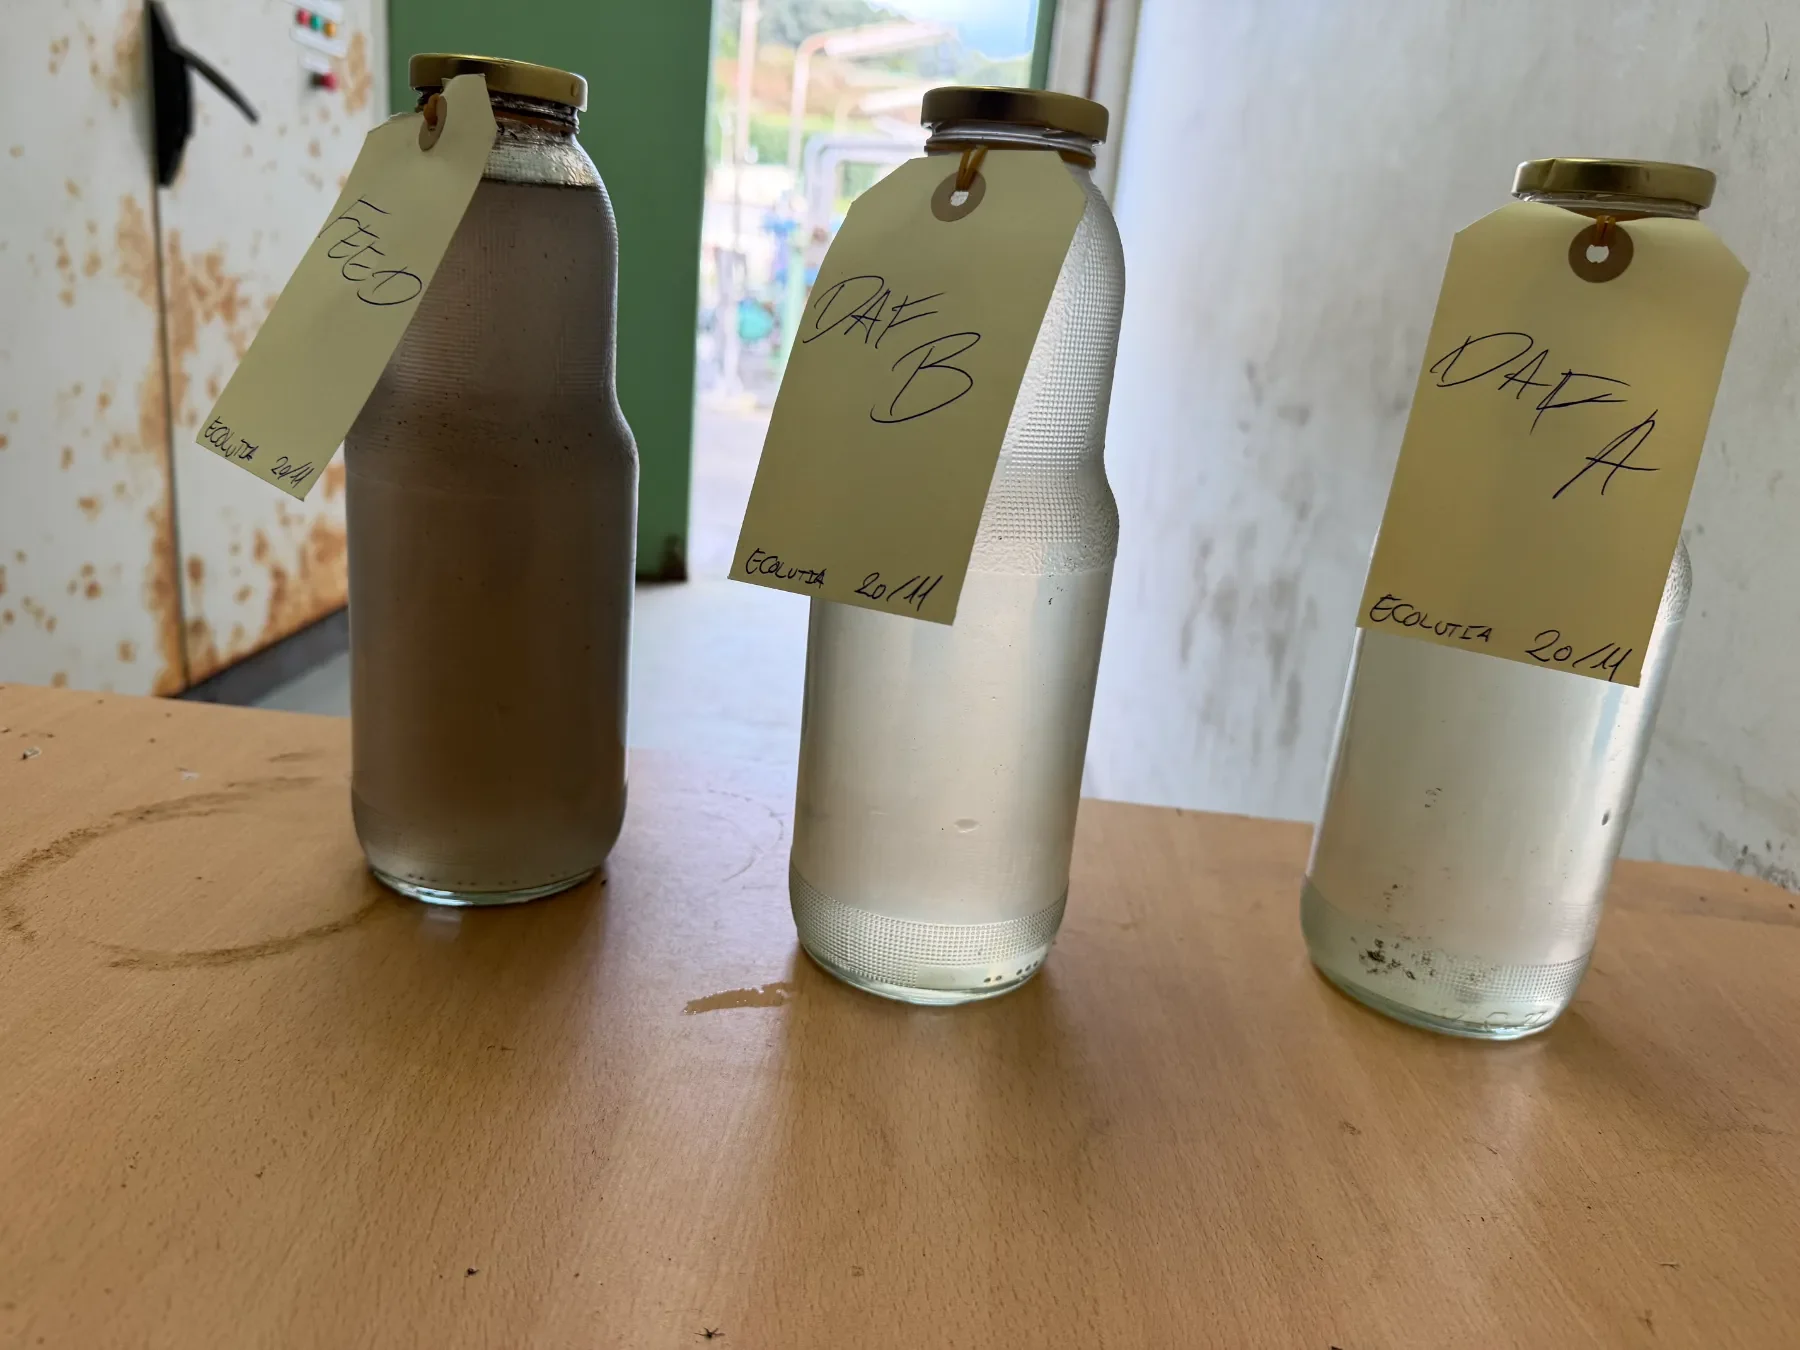
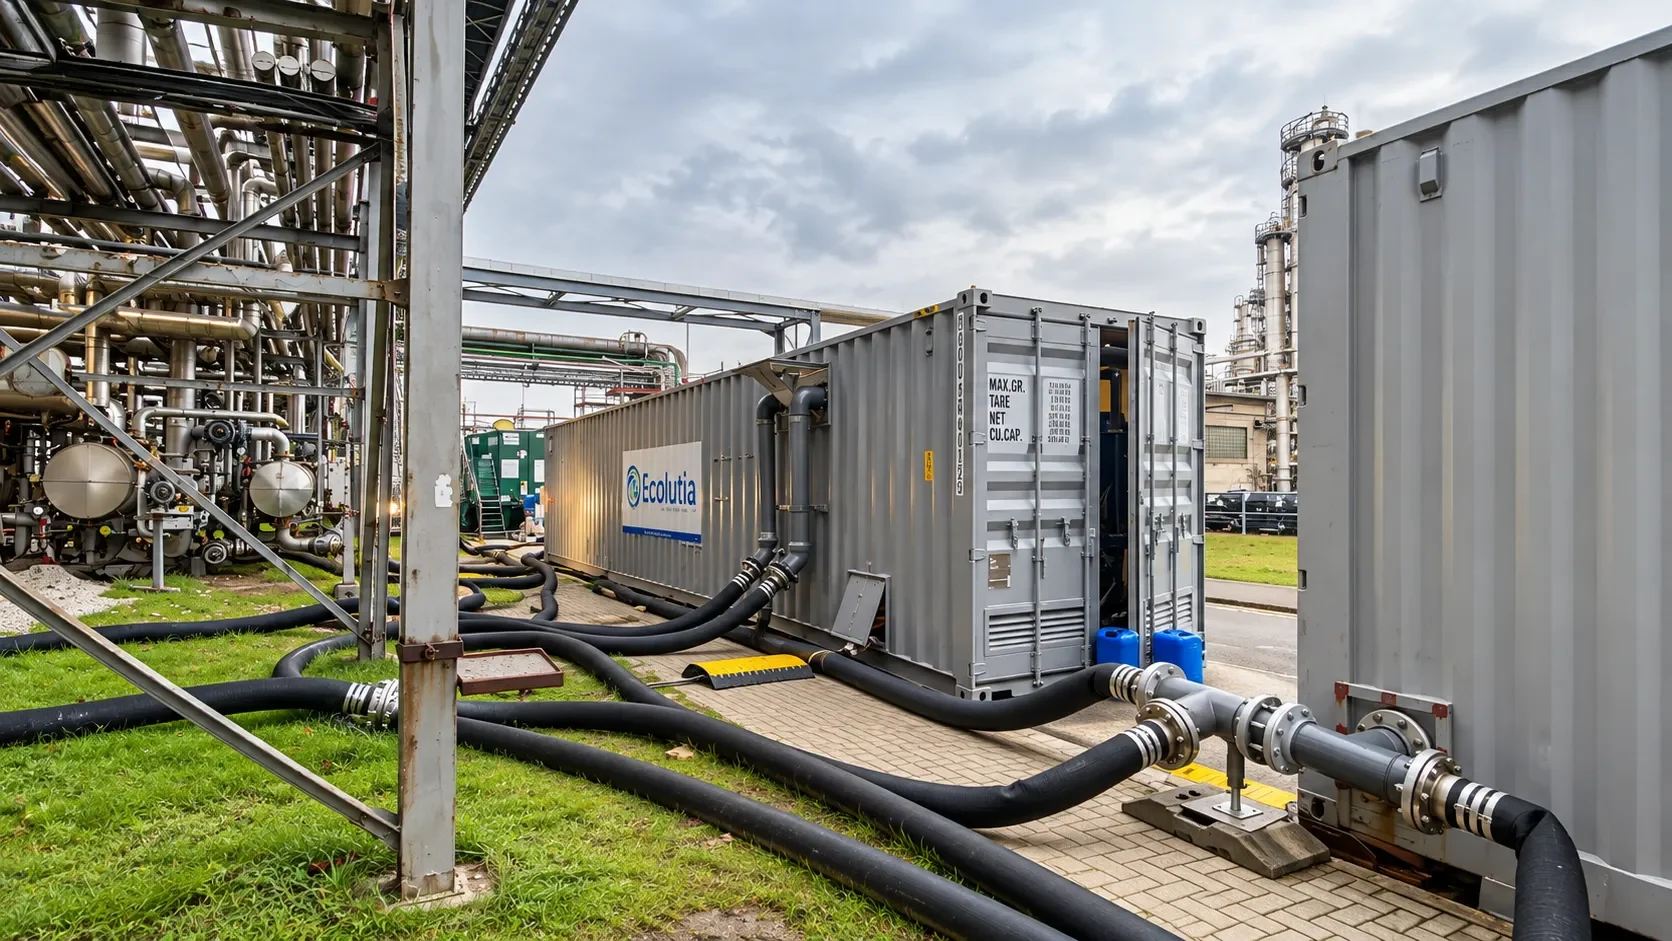
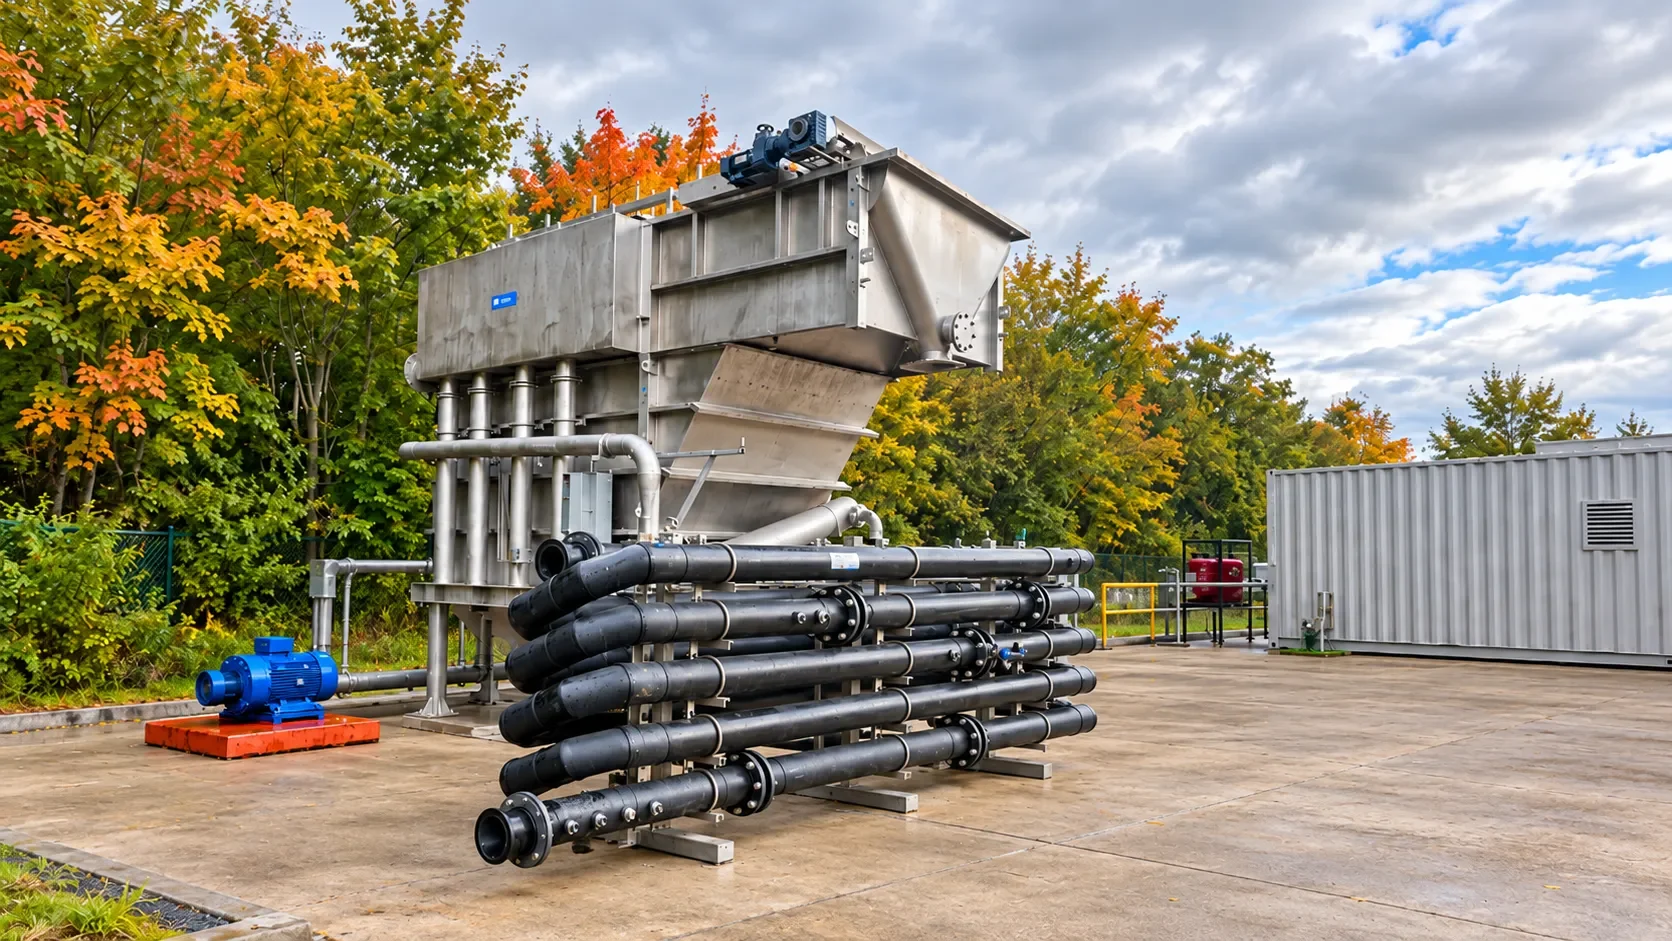
Ecolutia was able to rapidly deploy and integrate two DAFs, plug flow reactors and chemical dosing systems required for continuous operation of up to 310 m³/h, at a quality of less than 10 NTU, 10 ppm of oil and grease and 50 ppm TSS.
The commissioning and the engineering teams involved in the project found a suitable location and precise piping routing to minimise the extra ancillary equipment involved in using gravity to move product and waste. Also, the commissioning period was shortened thanks to good cooperation between the multiple teams involved.
During the project Ecolutia operations were regularly coordinated and communicated to the refinery engineers to ensure everybody remained involved and was aware of the work taking place.
One month scoped, three months delivered
Originally scoped as a one-month engagement, the project was extended by an additional two months to accommodate the customer’s evolving maintenance requirements — a testament to the flexibility and responsiveness built into every Ecolutia project.
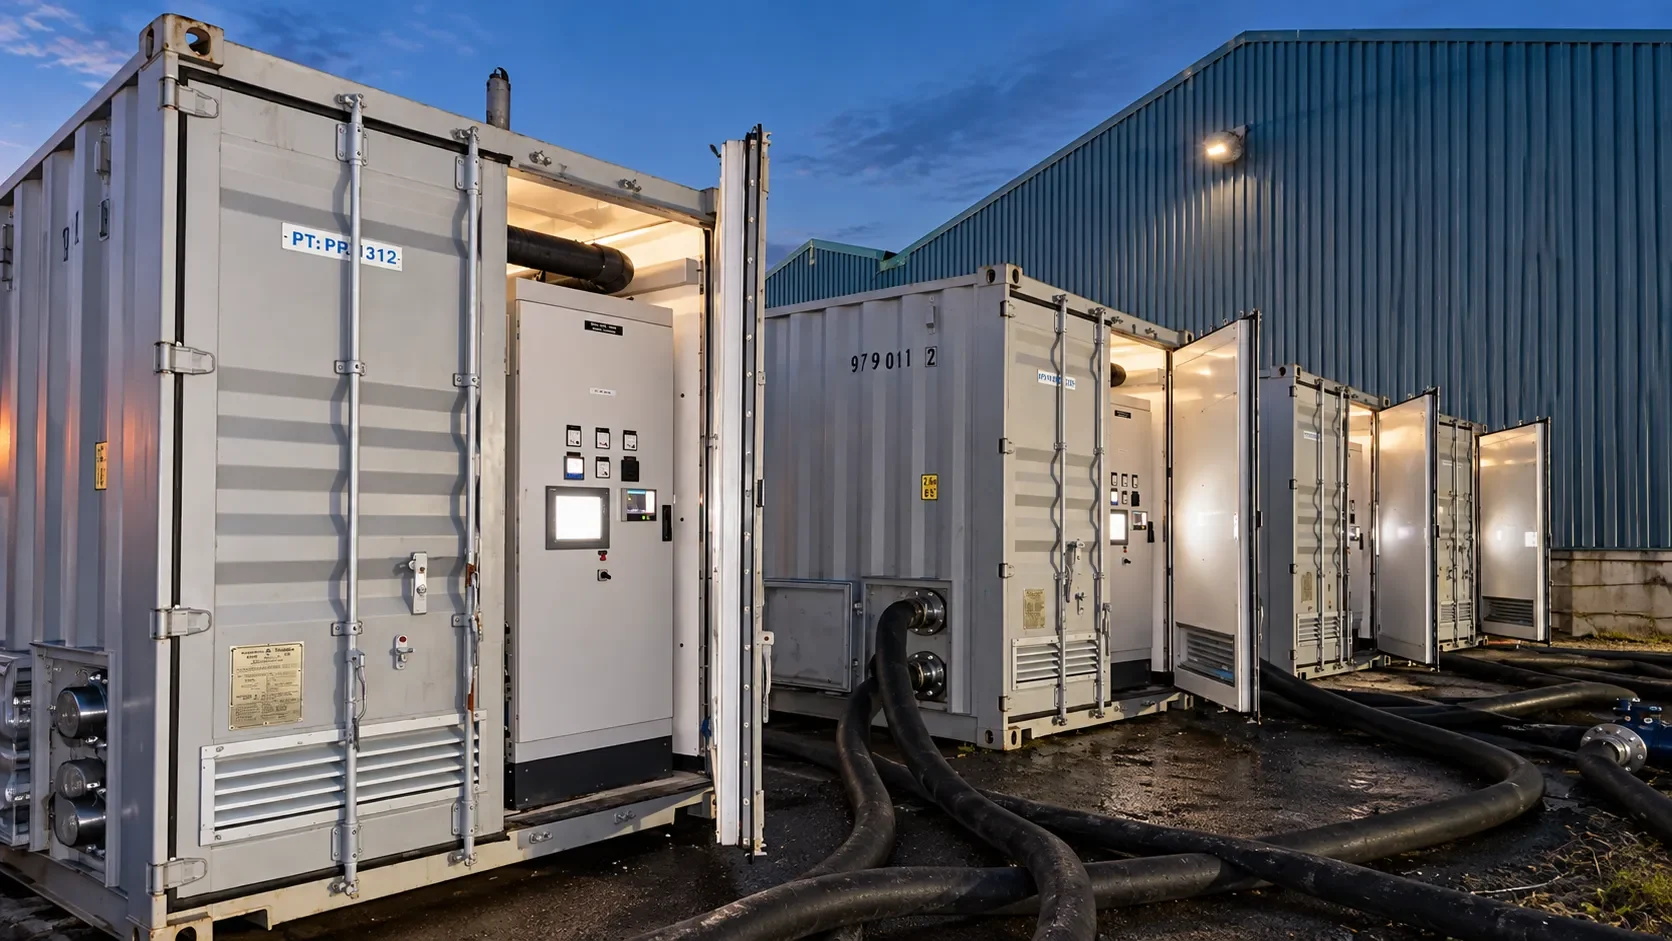
Throughout the entire engagement, the system consistently treated up to 310 m³/h, operating 24 hours a day, 7 days a week, while maintaining the quality standards agreed with the customer from day one. This unwavering reliability translated into minimal disruption and virtually no downtime to the customer’s process, freeing their team to focus on other critical on-site priorities rather than worrying about operational continuity.
Central to this success was Ecolutia’s remote monitoring system, which — combined with the deep technical expertise of the Ecolutia field service engineering team on-the-ground — enabled fast, informed responses whenever conditions changed. This proactive approach ensured that potential issues were addressed before they could escalate, resulting in smooth, uninterrupted operations throughout the three months.
The outcome: a fully successful project delivery that not only met but exceeded expectations, reinforcing the customer’s confidence in Ecolutia as a dependable long-term partner.